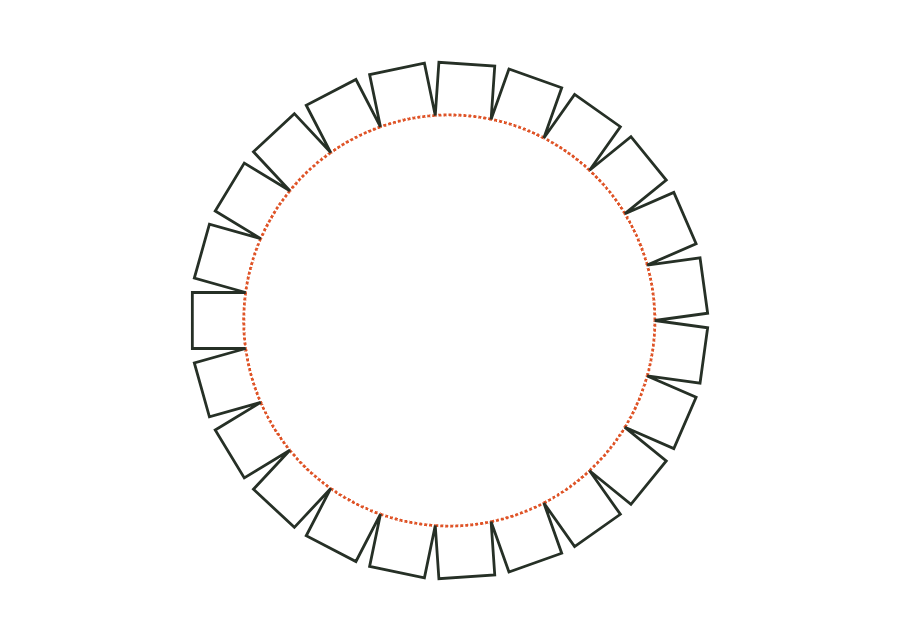
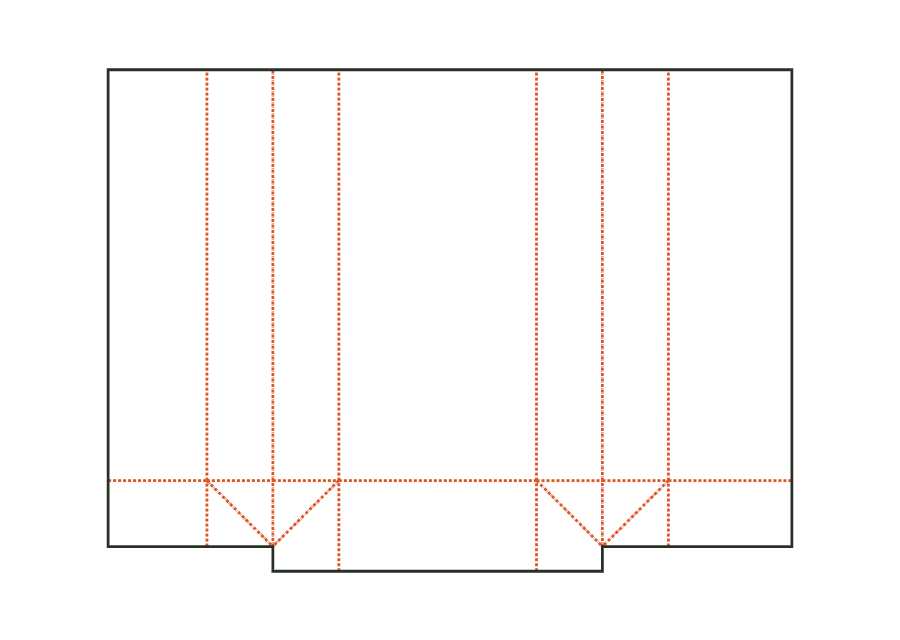
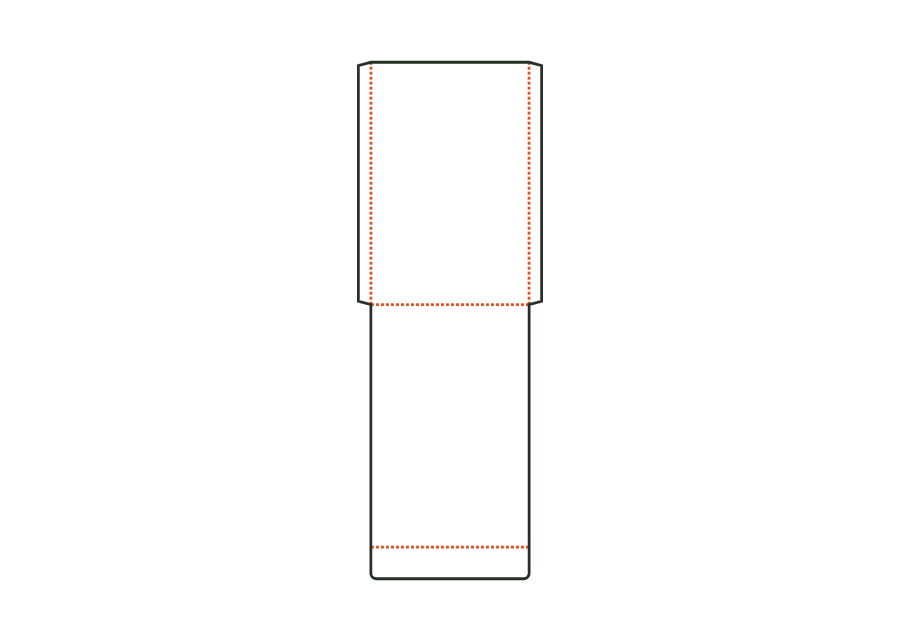Top turn-in
Strip above the top edge that folds into the tube; disable for cans.
 JetDieline
Cylinders and bags / JETDIELINE
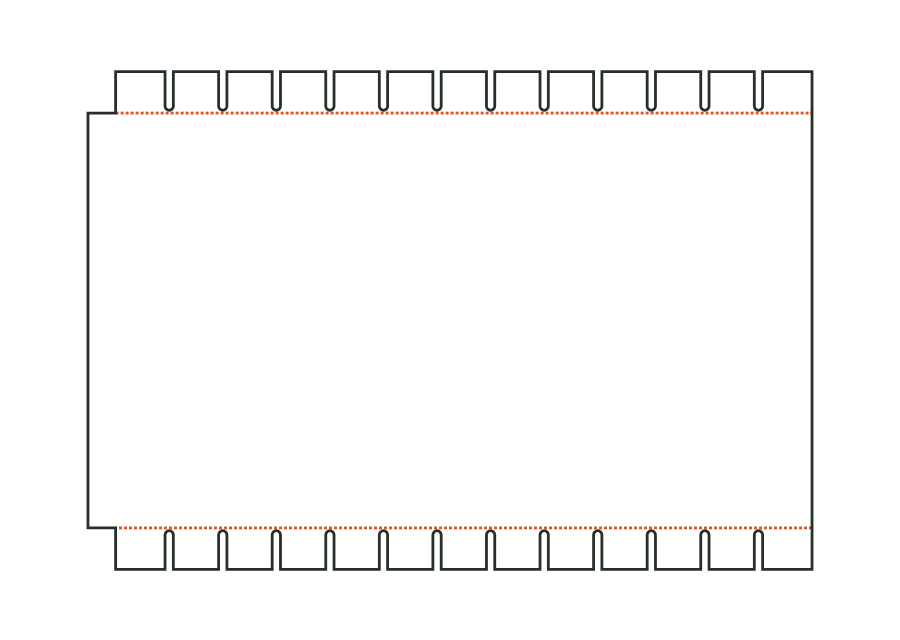
Calculate the wrap from diameter or circumference, height, and overlap. Slit turn-ins are added for a cardboard tube; for a can, you can disable both. The drawing shows the blank with starting values, not a finished can or confirmed fit.
Drag to rotate
03 / BOX
Simplified display model without material thickness, not to scale.
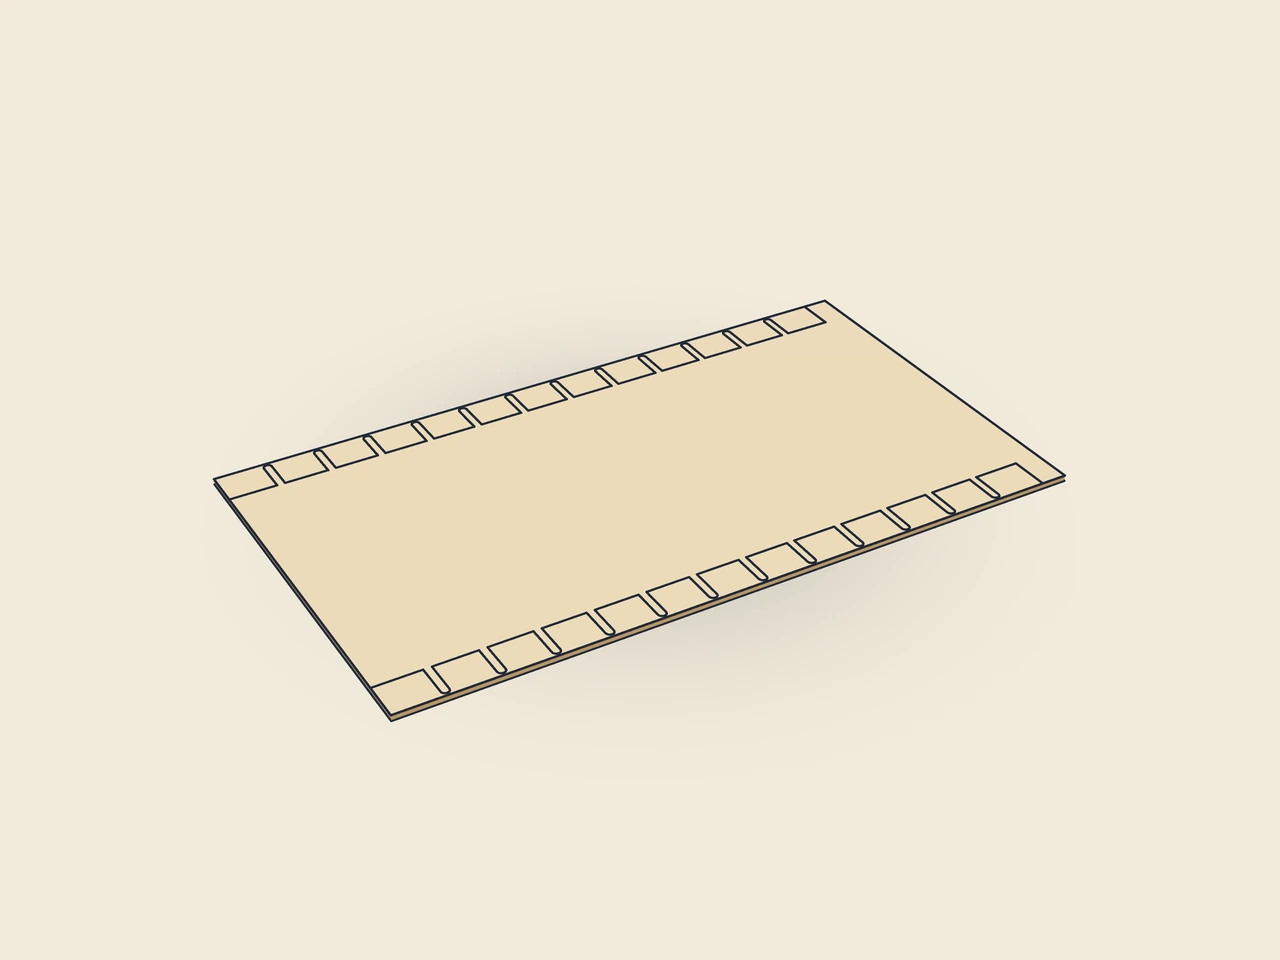
The 3D view is not available in this browser. The image shows the folded shape.
tube.wrapThe circumferential length accounts for the neutral fiber: π × (diameter + material thickness). Overlap is added. Top and bottom turn-ins lie outside body height. Slits divide the strips into flaps; a continuous bridge remains before the crease. Nominal flap width determines the rounded flap count.
Apply glue to the starting glue area and the reverse side, position the wrap's start along a generatrix, pull it taut around the body, and glue the end over the start. Pre-break turn-ins at the creases and fold them into the tube.
Test fit, folding and closure on a sample made from the intended material. Confirm material thickness, grain direction and production steps with your printer.
Outside dimension
These dimensions describe the preview, not a fixed packaging size. The app recalculates the dieline for your own dimensions.
Strip above the top edge that folds into the tube; disable for cans.
Strip below the bottom edge that folds into the tube; disable for cans.
Turn-in width from the crease; it extends over the tube wall into the interior.
Spacing of slits in the turn-in; flap count is rounded to fit the circumference.
In addition to body diameter, the blank accounts for material thickness at the neutral fiber. Glue overlap is then added. A simple rectangle with length π × diameter would omit both contributions. Compare the calculated wrap with the actual body and check seam fit on a sample.
Disable top turn-in and bottom turn-in. The corresponding slit strips are then removed from the blank. Body height and overlap remain input dimensions. For cardboard tubes, you can also turn in just one edge. Decide based on the tube structure and check the remaining edge with the production partner.
The desired flap width must be distributed around a closed circumference. The model therefore calculates a whole flap count and distributes the slits accordingly. Actual width may differ from the nominal value. The bridge before the crease holds the turn-in together; test whether flaps lie inside without interfering overlaps.
Find the right packaging shape and fit it to your product
Design the artwork directly on the real dieline
See problems before you pass on files
Files your printer can follow
The lid or base disc has glue flaps around a circular crease line. The starting dimensions are the inside diameter of the tube wall and its height. The parametric dieline shows the disc as an individual component; check a matching tube wall and assembly separately.
tube.discView templateThe flat bag consists of front and back with two glued side seams and a bottom fold. Enter bag width and height as outside dimensions. An optional flap on the back closes the opening; the dieline shows its effect on the paper blank.
bag.flatView templateThe side-gusset bag has a glued longitudinal seam and a block bottom made of flaps, ears, and triangles. You set bag width, gusset depth, and height. The inside dimension shown is converted into crease-to-crease dimensions using the material profile; the flat dieline also includes the bottom overlap.
bag.gussetView templateWith JetDieline, choose a suitable template, adjust its size, and place text, logos, and images directly on your packaging.
Try your dimensions