Glue flap
Width of the glue flap used to glue the blank into a tube. The material requires a minimum width.
 JetDieline
Folding cartons / JETDIELINE
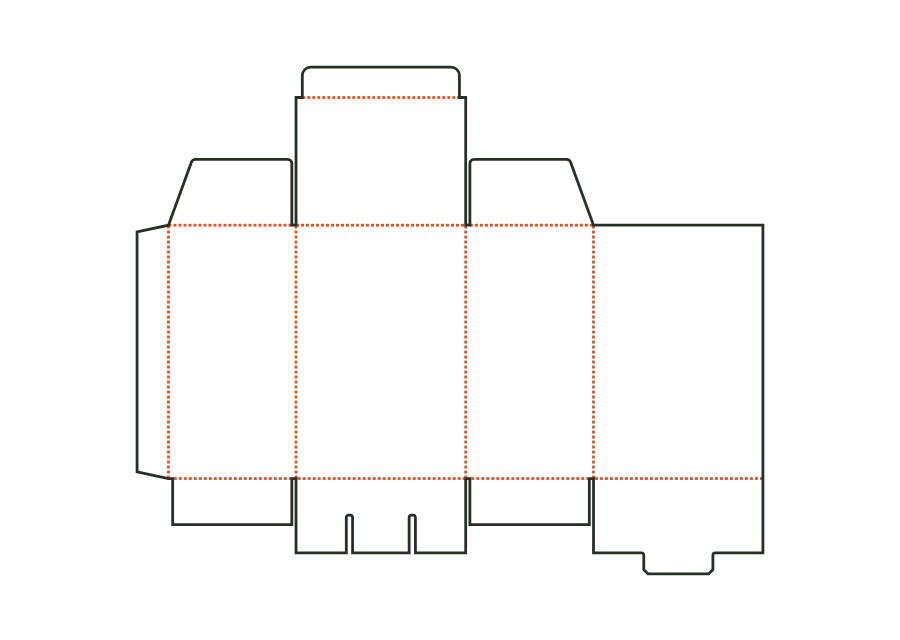
The snap-lock bottom closes with four interlocking flaps. Two side flaps lie inside; a tab at the back tucks under the tongue of the front flap. Version 1 combines this bottom with a tuck lid. The calculated example uses folding carton board 400 g/m² and shows the flat dieline with creases and bottom slits.
Drag to rotate
03 / BOX
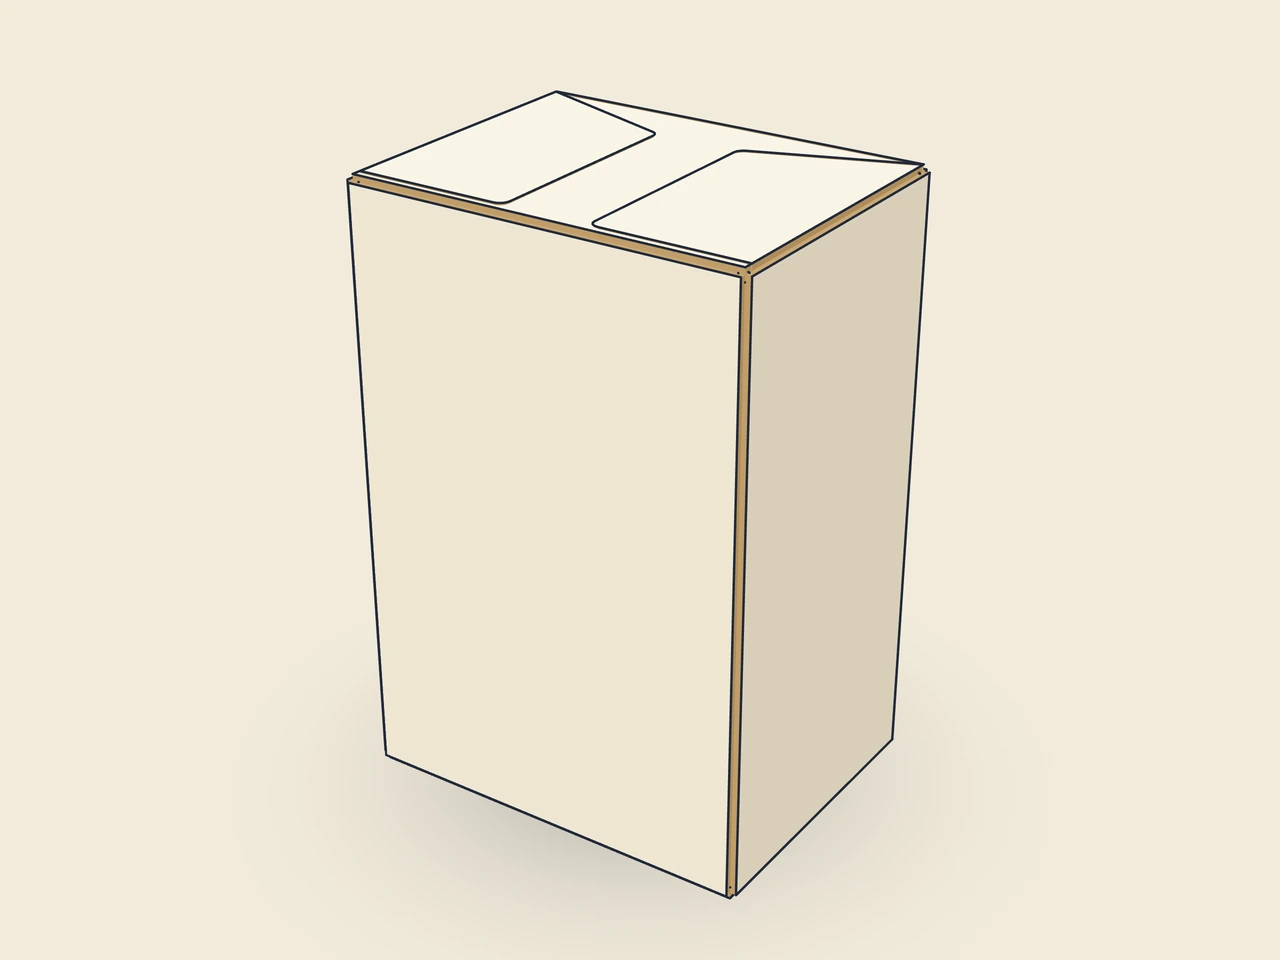
Simplified display model without material thickness, not to scale.
The 3D view is not available in this browser. The image shows the folded shape.
carton.snaplockThe body is glued at the side glue flap. To close the 1-2-3 bottom, fold the two side flaps, the slitted flap at the front, and the tab flap at the back in that order. The flaps change layers at the slits. The bottom locks without its own adhesive; the lid closes with dust flaps and a tuck flap.
Glue the glue flap and flatten the carton. Erect for filling, fold in side flaps 1 and 2, place flap 3 with the tongue over them, and tuck the tab of flap 4 under the tongue. After filling, fold in the dust flaps and insert the tuck flap.
Grain direction parallel to the height: wall creases lengthwise, bottom and lid creases crosswise; the flaps remain stiff and the tab does not bend out from under the tongue (check with the test print shop).
Test fit, folding and closure on a sample made from the intended material. Confirm material thickness, grain direction and production steps with your printer.
Inside dimension
These dimensions describe the preview, not a fixed packaging size. The app recalculates the dieline for your own dimensions.
Width of the glue flap used to glue the blank into a tube. The material requires a minimum width.
Bevel at the ends of the glue flap; facilitates folding and erection.
How far the tuck flap reaches into the box; at most approximately half the width (the height for the mailer).
Corner radius of the tuck flap; limited by half the flap width or tuck depth.
Side inset of the tuck flap relative to the lid, allowing easy insertion.
Fold the two side flaps inward first, then the front flap with the slits, and finally the tab flap at the back. The tab engages under the tongue; layers change at the slits. Check this sequence on the sample before filling, particularly with thicker board and small inside dimensions.
The bottom flaps interlock without their own adhesive. The side glue flap of the body is still glued to form a tube. This distinguishes the bottom from a preglued crash-lock bottom. You must perform the locking during erection; it does not happen simply by opening the flattened carton.
flapOverlap starts at 10 mm and has a range of 2 to 40 mm. The model also limits overlap to 40 % of bottom width. The maximum table value therefore does not fit every inside dimension. Coordinate overlap and tab length together and check the bottom with the target board.
Find the right packaging shape and fit it to your product
Design the artwork directly on the real dieline
See problems before you pass on files
Files your printer can follow
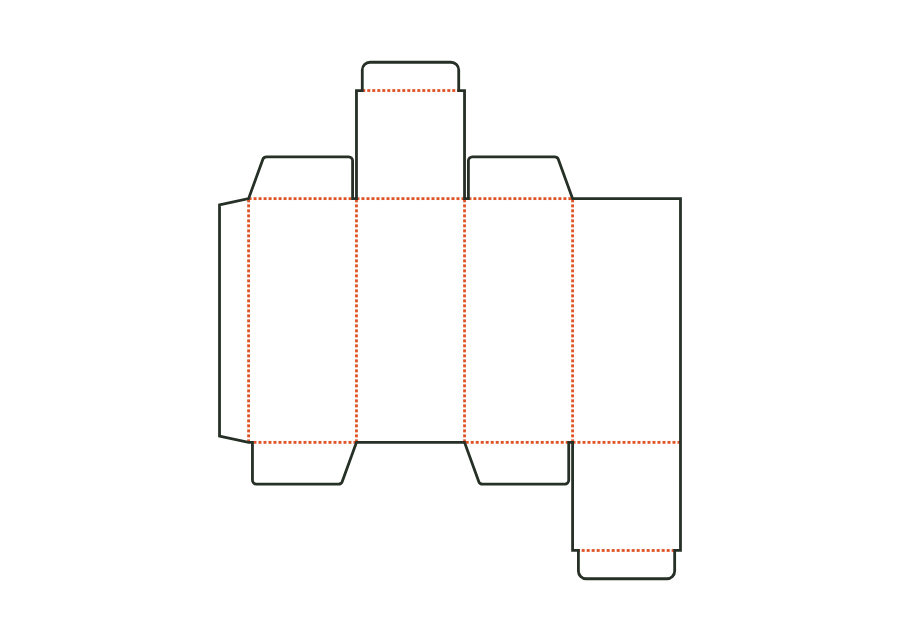
The top tuck flap is attached to the front, the bottom one to the back. The reverse tuck end carton calculates its walls, dust flaps, and closures from the inside dimension. The dieline shown comes from Version 3 with the hanging hole disabled; artwork, production dieline, and report can be exported together in the technical core.
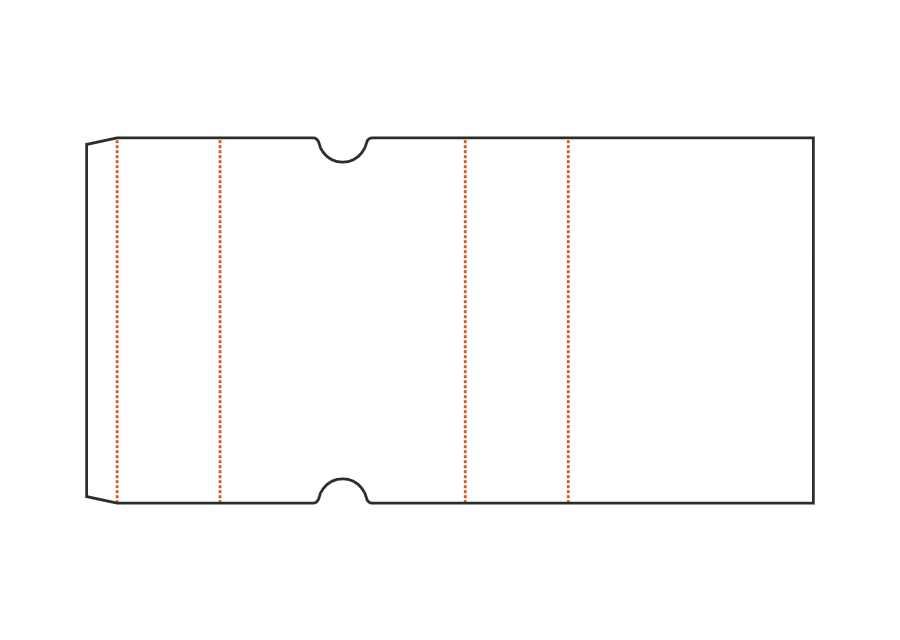
carton.tuckend.reverseView templateThe sleeve surrounds a product with four walls and remains open at both ends. Length and width describe the cross section; height denotes sleeve length. The dieline shows version 1 with finger notches on the front. Material thickness, glue flap, and notch position remain part of the calculation rather than simple scaling.
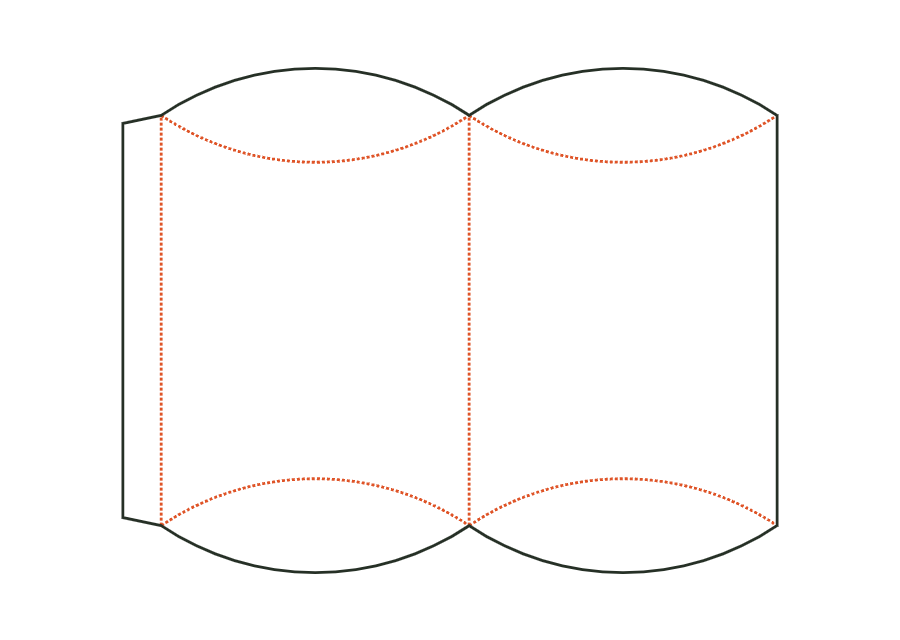
carton.sleeveView templateThe pillow box curves two wall surfaces between lens-shaped end flaps. Curved creases create the closure instead of straight lid creases. In version 1, the inputs mean the package's width × thickness × length. The shown dieline accounts for these proportions and the starting material; it does not define a rectangular box interior.
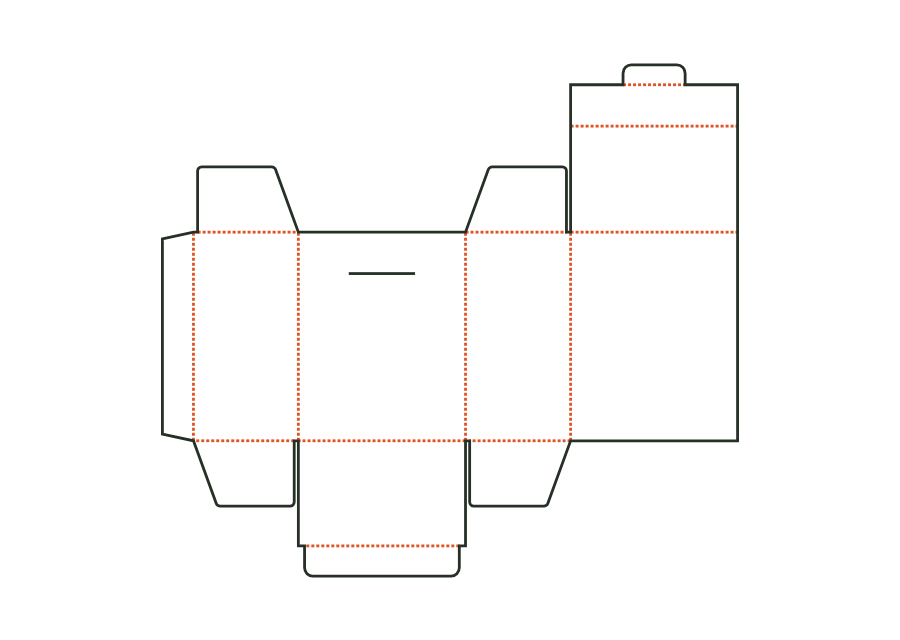
carton.pillowView templateThe hinged lid sits on the back wall and lays its front wall over the outside of the front. A lid flap inserts through a slot in the front; a tuck bottom closes the base. The page shows version 2 with the hanging hole disabled. The technical core calculates lid overhang, flaps, and creases from the chosen dimensions and material profile.
carton.hinged.lidView templateWith JetDieline, choose a suitable template, adjust its size, and place text, logos, and images directly on your packaging.
Try your dimensions